Food grade conveyor belts in Yorkshire
If your line moves anything destined for a plate, a bottle, or a wrapper, the belt underneath it isn't just equipment, it's part of your hygiene compliance.
Food grade conveyor belts are built for constant washdown, direct food contact, and the kind of scrutiny an audit brings.
If you're sourcing a replacement, planning a new line, or trying to work out whether your current belt actually meets the standard it needs to, here's what you need to know.
What is a food grade conveyor belt?
A food grade conveyor belt is made from compounds specifically approved for direct or indirect contact with food, most commonly food grade PVC, but also polyurethane (PU) and silicone belting depending on the application.
What separates these from standard industrial belts isn't just the surface, it's the whole compound: no plasticisers or additives that could migrate into food, and materials that hold up under repeated high-pressure washdown without breaking down or harbouring bacteria in the process.
Not every belt marketed as "food safe" is actually food grade in the regulatory sense. Standard PVC and food grade PVC can look identical side by side, but only one of them is manufactured to the compounds approved under UK and EU food contact regulations. If your facility runs audits, BRCGS, SALSA, or similar, that distinction isn't a nice-to-have, it's the thing an auditor will actually check.
Get the material and finish right and the belt becomes part of your hygiene system rather than a risk inside it. Get it wrong and you're looking at contamination risk, failed audits, or a belt that degrades fast under the exact washdown regime it was supposed to survive.
Benefits of food grade conveyor belts
Compliant by design
Manufactured from materials approved for food contact, so you're not relying on a standard belt "probably being fine."
Built for washdown
Handles regular high-pressure cleaning and the chemical exposure that comes with it, without the surface breaking down.
Non-porous surface
Doesn't hold onto moisture, residue, or bacteria the way a worn or incorrectly specified belt can.
Detectable options available
Metal-detectable and x-ray-detectable compounds exist for lines where a fragment of belt ending up in product is a genuine risk, common in bakery, meat, and ready-meal processing.
Colour options for visual safety
Blue is the industry standard colour for food grade belting, chosen because it rarely occurs naturally in food, so a torn fragment is easy to spot visually.
Multiple material options
PVC, PU, and silicone each suit different environments, wet processing, high-temperature lines, or chilled and frozen handling.
Supports HACCP and audit compliance.
The right belt is one less thing flagged in a hygiene audit, not a recurring line item.
Resists odour transfer
A non-absorbent surface means one product's smell or flavour doesn't carry over to the next batch run across the same line, useful on multi-product facilities switching between runs
Common industries
Industries that use food grade conveyor belts
Bakery and confectionery
Dough, baked goods, and packaged confectionery moving through production and packing lines where hygiene and washdown are constant.
Meat and poultry processing
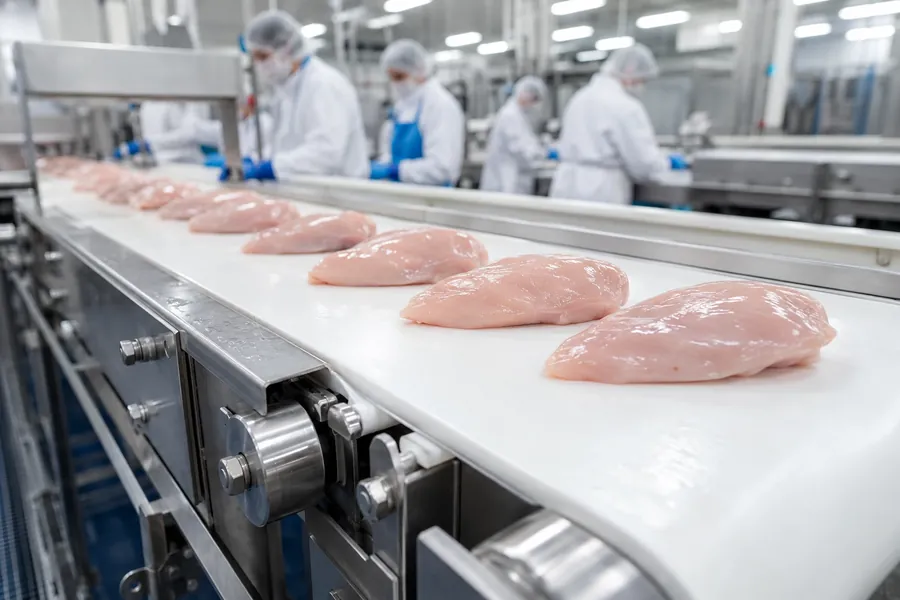
High-hygiene environments with frequent washdown, often requiring detectable belt compounds as standard.
Dairy production
Processing and packing lines where chemical washdown resistance and non-porous surfaces both matter.
Ready meals and prepared foods
Multi-ingredient lines where cross-contamination risk makes belt hygiene a daily concern, not just an audit-week one.
Beverage and bottling
Soft drinks, juices, and dairy-based beverages moving through high-speed filling and bottling lines, where constant moisture exposure and frequent washdown between batches are part of daily operation, not an occasional deep clean.
Fruit and vegetable packing
Washdown-heavy environments, often with lighter loads but high line speed.
Fish and seafood processing
Cold, wet conditions combined with strict hygiene and odour-resistance requirements.
Pharmaceutical and nutraceutical
Cleanroom-adjacent production where hygiene compliance overlaps directly with food-safety standards, tablet coating, supplement manufacturing, and similar processes where surface integrity and washdown resistance matter as much as they do on a food line.
Choosing the right food grade conveyor belt
Getting food grade belting wrong doesn't just cost you belt life, it's a compliance risk.
Here's what to get right.
Why choose Yorkshire Conveyor Belts?
We make finding the right conveyor belt specialist simple.
Finding the right supplier shouldn't mean ringing five different companies or hoping you've found the right one.
We're not a supplier.
We connect Yorkshire businesses with conveyor belt specialists who are, people who supply, install, and maintain food grade belting across the region and understand the difference between "food safe" as a marketing phrase and food grade as a regulatory standard.
Tell us what you need and we'll match you with someone who can actually help.
We cover Leeds, Sheffield, Bradford, Hull, Doncaster, Wakefield, and the wider Yorkshire area.
Why businesses use us
🏆Trusted local specialists
Vetted conveyor belt experts across Yorkshire.
⚡24-hour response
Fast replies when production can't wait.
🛡No obligation
Advice first. Decide when you're ready.
🏭Industrial expertise
Warehousing, manufacturing, food and logistics.
🏭Fast, simple process
Complete one 2-minute survey
✔Right specification
We help you avoid costly mistakes.
📍Yorkshire coverage
Leeds, Sheffield, Hull, Bradford, Doncaster and beyond.
Still need help choosing the right belt?
Food grade conveyor belt FAQs
Need a food grade conveyor belt in Yorkshire?
What are food grade conveyor belts used for?
Any application where the belt has direct or indirect contact with food, bakery, meat and poultry, dairy, ready meals, beverage bottling, and fruit and vegetable packing among the most common. Anywhere hygiene compliance is a daily operating requirement, not an occasional check.
What's the difference between food grade and standard conveyor belts?
Material composition and regulatory approval. Food grade belts use compounds specifically approved for food contact under UK and EU regulations, standard belts don't, even if they look identical on the surface. If your facility runs hygiene audits, this distinction is exactly what gets checked.
Do food grade belts need to be a specific colour?
Not by law, but blue is the industry standard for a practical reason: it's a colour that rarely appears naturally in food, so a torn or worn fragment is much easier to spot visually or catch on a detection system.
What is a metal-detectable conveyor belt?
A belt manufactured with a compound that shows up on metal detection equipment, so if a fragment breaks off during processing, it can be caught before product reaches packaging. Common on bakery, meat, and ready-meal lines where fragment risk is a real concern.
How often do food grade belts need replacing?
Shorter than a standard industrial belt in most cases, because of the constant washdown and chemical exposure they're built for. Actual lifespan depends heavily on the washdown regime, the material chosen, and how well tracking and tension are maintained, a specialist reviewing your specific line will give a far more accurate answer than a generic figure.
What maintenance does a food grade conveyor belt need?
Beyond the standard tension and tracking checks any belt needs, food grade belts should be inspected specifically for surface degradation from cleaning chemicals, and for any small tears or delamination that could create a hygiene risk rather than just a mechanical one. Regular inspection matters more here than on a standard industrial line.
What certification do food grade conveyor belts need?
Food grade conveyor belts need to be manufactured from materials approved for food contact under UK and EU regulations, that's the baseline, not an optional extra. Beyond that, the specific paperwork you need depends on your own facility's audit standard. If you run BRCGS, SALSA, or a similar scheme, your auditor will expect material traceability and documentation confirming the belt's compliance, not just a supplier's word that it's "food grade." The safest approach is asking for that paperwork upfront, before the belt arrives on site, rather than after an audit flags a gap.
Replacement belt, splicing, repair, or a full conveyor project, whatever you're dealing with, we can connect you with a Yorkshire food grade belt specialist who can help. Tell us what you need.
Need a conveyor belt specialist in Yorkshire?
Answer a few quick questions and we'll connect you with the right local specialist.
Start your 2-minute survey✓ No obligation • ✓ Response within 24 hours